dyyseo

What are nanoparticles?


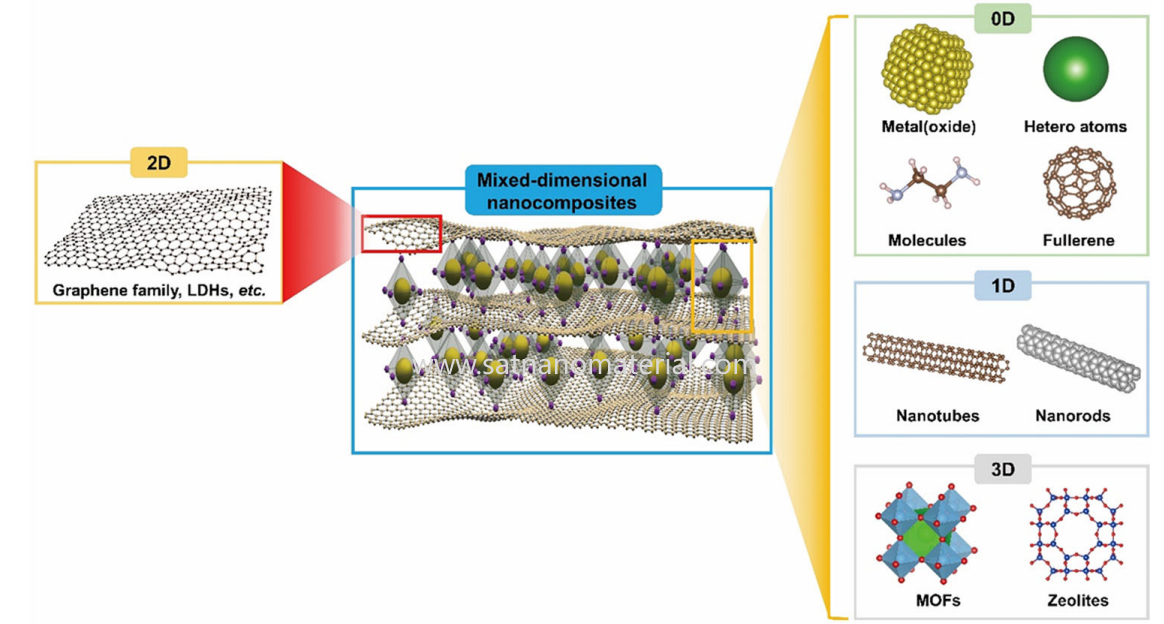
Nanoparticles (NPs) are typically defined as granular materials with at least one dimension at the nanoscale (1-100 nm) in three-dimensional space. From the dimensions of structure and morphology, nanoparticles can be classified into zero dimensional nanomaterials (0D nanomaterials), corresponding to one-dimensional (1D) and two-dimensional (2D) nanomaterials. 0D nanoparticles are subject to size constraints in three-dimensional space, with typical representatives including metal nanoparticles, oxide nanoparticles, sulfide nanocrystals, etc. In addition, based on their composition, nanoparticles can be further subdivided into single component structures (such as pure metals, single oxides) and multi-component structures (such as core-shell structures, alloy nanoparticles, heterostructures, etc.), and their structural complexity directly affects their functional performance.

powder aggregation


What is nanoparticle aggregation and dispersion?


Nanoparticle aggregation: refers to the phenomenon of primary nanoparticles forming larger particle aggregates through physical or chemical forces, usually manifested as size growth and a decrease in specific surface area. Agglomeration can be divided into two categories: reversible agglomeration and irreversible agglomeration. The former can be redispersed through external intervention such as ultrasound or solvent adjustment, while the latter is often caused by consolidation, sintering, or chemical bonding, making it difficult to restore the original dispersed state. Nanoparticle dispersion: refers to the uniform distribution of nanoparticles in liquid, solid, or gas media, maintaining effective spacing between particles, avoiding contact aggregation, and maintaining their monodispersity and high specific surface area state. Effective dispersion is a prerequisite for unleashing its nano effect.

powder aggregation

SAT NANO is a best supplier of nano powder and micro powder in China, if you have any enquiry of nanoparticle aggregation and dispersion, please feel free to contact us at admin@satnano.com


Why modify the powder?


Inorganic powders have hydrophilic and polar surfaces, but poor compatibility with organic matrices (plastics, rubber, resins). Direct use can lead to poor performance, so modification is necessary.
(1) Improve dispersibility and prevent agglomeration. Inorganic powders with a large specific surface area are prone to agglomeration, which can lead to defects and a decrease in material strength and poor appearance. The modified powder is uniformly dispersed without clumping.
(2) Improve compatibility with organic matrices. Powder surfaces are hydrophilic (polar), while plastics, rubber, and resins are hydrophobic (non-polar). Direct mixing results in poor interfacial bonding, similar to "sand mixed with butter". After modification, the surface of the powder becomes lipophilic and tightly adheres to the resin.
(3) Enhancing interfacial adhesion and improving mechanical properties, the modified powder forms chemical bonds or strong adsorption with the resin, which can significantly improve tensile strength, impact strength, bending strength, hardness, wear resistance, etc.
(4) Reducing the oil absorption value and improving the processing flowability of unmodified powder can lead to a significant increase in resin viscosity, processing difficulties, and inability to increase the amount of filler added. After modification, the oil absorption value decreases, allowing for high filling and cost reduction.
(5) Improve weather resistance, water resistance, and corrosion resistance to reduce powder water absorption, enhance coating acid and alkali resistance, and improve material aging and yellowing resistance.
(6) Improve electrical and thermal performance, enhance insulation, improve thermal conductivity (such as modifying thermal conductive fillers), and improve flame retardant efficiency (magnesium hydroxide/aluminum).
(7) Improve surface gloss, hand feel, color, commonly used in coatings and plastics to make products more delicate, shiny, and have a better hand feel.

(8) To prevent powder oxidation, self ignition, and reaction, especially for metal powders (aluminum powder, zinc powder), modification can prevent oxidation and self ignition, and improve storage stability.


Which powders need to be modified?


1. Functional powders: titanium dioxide (titanium dioxide), iron oxide red, iron oxide yellow, iron oxide brown, iron black, pearlescent mica, white carbon black, carbon black, nano zinc oxide, hollow glass microspheres, calcium sulfate whiskers, calcium carbonate whiskers, active calcium silicate, flake zinc powder, aluminum tripolyphosphate anti rust pigment, etc;
2. Flame retardant powders: magnesium hydroxide, aluminum hydroxide, etc;
3. Ceramic powders: alumina, zirconia, aluminum nitride, silicon nitride, silicon carbide, barium titanate, strontium titanate, magnesium titanate, zinc titanate, cordierite, magnesium olivine powder, etc;
4. Magnetic powders: neodymium iron boron magnetic powder, strontium ferrite/barium ferrite, iron silicon aluminum, carbonyl iron powder and other soft magnetic powders, nano iron oxide, etc;
5. Carbon materials: graphite, graphene powder, carbon fiber powder, carbon nanotubes, etc;
6. New energy powders: ternary materials, lithium iron phosphate, lithium cobalt oxide, natural/artificial graphite, silicon-based negative electrode, lithium titanate, boehmite, lithium hexafluorophosphate, expandable graphite, zinc borate, silver powder, etc;
7. Metal powders: aluminum powder, zinc powder, copper powder, iron powder, etc;
8. Cosmetics ingredients: silicon dioxide, titanium dioxide, zinc oxide, iron oxide red, iron oxide yellow, iron oxide black, chromium green, ultramarine, manganese violet, hydroxyapatite, etc;
9. Thermal conductive fillers: gold powder, silver powder, copper powder, tin powder, metal nanowires, aluminum oxide, hexagonal boron nitride, silicon carbide, zinc oxide, nanodiamonds, etc.

SAT NANO is a supplier of ceramic powders including alumina, zirconia, aluminum nitride, silicon nitride, and silicon carbide. We can provide surface treatment for these products. Surface modification technology is a key means to improve the performance of ceramic powders. Regarding the five ceramic powders you mentioned, key properties such as strength, toughness, hardness, and hydrolysis resistance of the final ceramic products can be significantly improved through processes such as coupling agent modification and surface coating.
The following is a summary of the specific enhancement data in terms of mechanical and process properties of these five ceramic powders after surface modification:

Ceramic powder Surface modification methods
solid content
Enhanced data (compared to unmodified samples)
aluminum dioxide Silane coupling agent A151 modification
- • Hardness: 85.5 HD
• Tensile strength: 52.36 MPa
• Impact strength: 10.12 kJ/m ²


Surface coating of aluminum chloride/aluminum based complex
- Stamping mechanical strength: increased from a maximum of 35 MPa to 51 MPa (an increase of approximately 45.7%)
zirconia
Polymer dispersant KOS110 modification
46.5%
Vickers hardness: 1814 HV
• Shrinkage rate: 21.9%

Laser microtexture+silane modification
- Surface water contact angle: from hydrophilic to 159.6 ° (superhydrophobic)
aluminum nitride
Surface esterification reaction of lauric acid (LA)
- Hydrolysis resistance: The modified powder is placed in water at 40 ℃ for 72 hours, with a stable pH value below 9 and no phase transition occurring
silicon nitride
Low melting point glass powder coating
20% • Bending strength: increased by up to 14.3%
• Fracture toughness: up to 31.1% improvement

Hydroxylation+silane coupling agent KH560 modification
50% Bending strength: (407.95 ± 10.50) MPa
Fracture toughness: (4.38 ± 0.45) MPa · m ^ {1/2}
silicon carbide
Microwave plasma modification (MPM)

Surface hardness: significantly reduced from 37.04 GPa to 4.71 GPa

Analysis of Modification Effect and Mechanism


In addition to direct data augmentation, different modification methods can also solve specific problems from a mechanistic perspective:

Aluminum oxide (Al2O3) - strength and interface compatibility: By coating the surface with aluminum chloride, the pore structure of the aluminum oxide matrix can be effectively filled, increasing the density and thus increasing the stamping mechanical strength from 35 MPa to 51 MPa. By using silane coupling agents for modification, the interface bonding between nano alumina and resin matrix can be improved, making it a reinforcing phase that significantly enhances the hardness and tensile strength of photosensitive resin.

Zirconia (ZrO2) - High hardness and functionality: By modifying ZrO ₂ powder with polymer dispersants, high solid content and low viscosity 3D printing slurries can be prepared. After sintering, the Vickers hardness of the ceramic can reach 1814 HV, demonstrating excellent mechanical properties. In addition, through laser chemical treatment, micro nano structures can be constructed on its surface and low surface energy substances can be grafted to obtain a superhydrophobic surface with a contact angle of up to 159.6 °, expanding its applications in self-cleaning and other fields.

Aluminum Nitride (AlN) - Hydrolytic Stability: AlN is highly reactive with water, leading to a decrease in performance. Using lauric acid for surface modification, its carboxyl group undergoes esterification reaction with the hydroxyl group on the AlN surface, forming a dense coating layer (with a thickness of about 12.2-16.1 nm). This barrier can effectively prevent the diffusion of water molecules, keeping the pH value of the modified powder below 9 even after being placed in water for 72 hours, greatly improving its storage and processing stability.

Silicon nitride (Si3N ₄) - comprehensive mechanical properties: By coating modification with low melting point glass powder, the glass phase formed during sintering can refine the grain size, and the fracture toughness can be increased by up to 31.1% through toughening mechanism. The modification of silane coupling agent KH560 can improve the compatibility between powder and resin, reduce the viscosity of the slurry, and achieve a solid content of 50 vol%. At the same time, the flexural strength after sintering exceeds 400 MPa.

Silicon carbide (SiC) - improved processing performance: The extremely high hardness of SiC makes it difficult to process. By microwave plasma modification, a relatively soft SiO2 modified layer can be generated on the surface of SiC, causing its surface hardness to drop sharply from 37.04 GPa to 4.71 GPa, thereby changing the material removal method from brittle fracture to plastic removal, greatly improving the efficiency and surface quality of subsequent polishing (roughness Ra can reach 0.31 nm).


From the above data, it can be seen that the surface modified products provided by SAT NANO have a significant increasing effect. If you have any enquiry, please feel free to contact us at admin@satnano.com

Why do nanoparticles aggregate?

1.Surface free energy driven mechanism


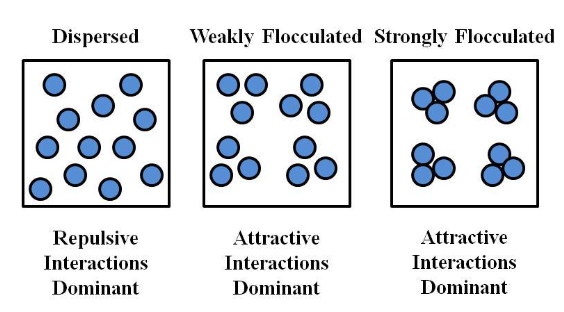
Nanoparticles have a larger specific surface area and unsaturated surface atoms, leading to an increase in surface free energy. Multi particle contact can reduce the total surface area, release interfacial energy, and thus lower the system's free energy. This trend of energy minimization is the intrinsic thermodynamic driving force behind the spontaneous agglomeration of particles and is a common source of agglomeration at the nanoscale.
nanoparticles aggregate


2.Static electricity and electrical double-layer instability


The electric double-layer formed by charged particles can provide a stable dispersion state of electrostatic repulsion. When the pH approaches the isoelectric point or the ionic strength increases, the bilayer is compressed, the repulsive force decreases, and the attractive potential energy between particles dominates, leading to agglomeration. The stability of this potential barrier determines the anti aggregation ability of the system.

nanoparticles aggregate


3.The influence of solvent medium action


Particles in solution rely on solvation shell to achieve interface stability. If the solvent has weak polarity and poor affinity, it is difficult to form an effective solvation layer, which increases the direct contact between particles, enhances van der Waals forces, and triggers agglomeration. Therefore, the physical and chemical properties of solvents directly affect the dispersion state of particles.


4.Chemical binding aggregation mode


Particles with high reactivity can form stable clusters through hydrogen bonding, coordination, or covalent bonding of functional groups such as hydroxyl and carboxyl groups on their surfaces. This chemical bonding makes aggregation irreversible and difficult to physically dissociate. This process is based on the chemical reactivity of surface energy states and functional groups.

nanoparticles aggregate


Why are nanoparticles dispersed?

1. Establishing a potential energy barrier through electrostatic repulsion

The surface charge of particles will form an electric double layer structure in liquid, and when two particles approach, electrostatic repulsion will be generated between the electric double layers. This repulsive effect can build a potential energy barrier between particles, effectively suppressing aggregation caused by short-range attraction. If there is a sufficiently high potential barrier in the total potential energy of the system, the particles are in a dynamically stable state. This mechanism relies on charge density, dielectric constant, and ionic strength, and is a common stable basis for water-based colloids.

nanoparticles aggregate

2.Space steric hindrance effect enhancement interval


The steric hindrance effect is generated by the adsorption or grafting of polymer segments on the surface of particles. When particles tend to approach, these molecular structures generate conformational compression and repulsion forces, preventing particle contact.
This mechanism does not rely on surface charge and is suitable for high ionic strength or non-polar systems. Spatial hindrance provides a physical barrier and is one of the most common dispersion mechanisms in polymer coated or surfactant systems, particularly evident in surface modified particles.

nanoparticles aggregate


3.Solvation shell impedes contact


When particles form a stable solvation layer with solvent molecules, this layer provides significant energy barriers when particles approach, preventing direct contact between particles. The thickness and stability of the solvation layer depend on the polarity, hydrogen bonding ability, and affinity with the particle surface of the solvent. If the contact between particles needs to overcome the desorption energy of the solvation layer, this energy barrier can effectively reduce the probability of agglomeration and is an important dispersion guarantee mechanism under non electric repulsion conditions.
nanoparticles aggregate


4.Surface functionalization enhances chemical stability


Surface functionalization can introduce charge, spatial structure, or hydrophobic regulatory factors to enhance particle repulsion or improve interfacial compatibility, thereby improving dispersion stability. By grafting ligands, polymer chains, or functional groups, the surface can achieve a dual mechanism of electrical repulsion and spatial protection, making it difficult for particles to approach and form aggregates. This method is widely used in systems such as metal oxides and quantum dots, and is one of the core strategies for achieving controllable dispersion.


SAT NANO is a best supplier of nano powder and micro powder in China, we can supply metal powder, alloy powder, oxide powder and carbide powder, if you have any enquiry, please feel free to contact us at admin@satnano.com


XRD is an important means of characterizing phases. Strictly speaking, it can determine the existence of a certain phase, but cannot determine the absence of a certain phase, making it easier to distinguish between truth and falsehood.

So, what is its detection limit?

Firstly, we must emphasize that XRD analysis of elemental content is very inaccurate. If we have to say what the detection limit is mainly determined by, it is determined by the power and tube current of the instrument. If we want to characterize the elemental content, it is best to use chemical methods or atomic absorption spectroscopy.


In addition, the detection limit of XRD cannot be simply expressed in%, which is closely related to the dispersion of the detected substance, that is, the crystallinity, and the type of substance. The mass absorption coefficient of the sample is large, and the detection limit will be much higher.


If a detection limit must be determined, it is generally around 5%. However, different phases have varying absorption of X-rays, resulting in significant differences in detection limits. Like elemental silicon, it can generally be detected at around 1%, while other phases, up to 10%, may be difficult to detect. Of course. Under the same sample conditions, using higher diffraction power and longer scanning time will yield better results. However, if you want to extend the scanning time, extending it by one or two times will not yield any results.


Experience has shown that if a conventional scanning speed can detect any signs of existence, then scan at a speed of 1 degree/min or slower. If you can't see any traces at regular scanning speeds, there's no need to put in any more effort. Conducting semi quantitative analysis is indeed very inaccurate, and the results are indeed related to grain size. The precipitation phase with small grain size is difficult to detect, let alone perform quantitative analysis. The phase with small grain size will increase its RIR value. The RIR value of CeO2 has been studied, and the RIR values of the products at different temperatures differ by 10 times.


SAT NANO provides two examples to illustrate:


Example 1: A diamond sample was contaminated with silver, and a silver peak appeared in the XRD spectrum, which was very obvious. Through quantitative calculation, it was found that 0.04% wt of silver was present in the sample. To further confirm, spectral analysis revealed the presence of 0.038% wt silver.

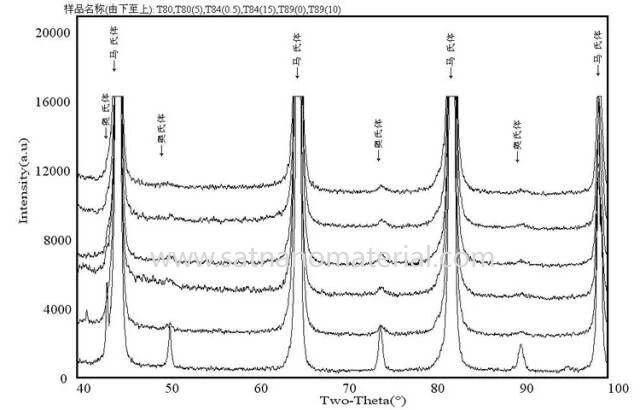
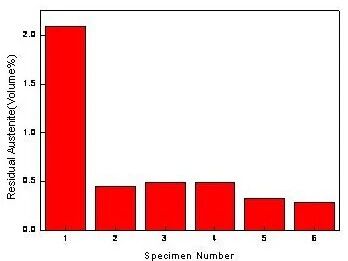
Example 2: The steel sample contains a small amount of residual austenite, and the transformation from austenite to martensite is measured after tensile fracture. The sample contains both austenite and martensite phases. The residual austenite in the sample before stretching is about 2% (V), and after the tensile test, only 0.2% to 0.5% austenite remains in the sample. According to the conventional scanning speed (8 °/min), no austenite peak can be found in the scanned spectrum. Later switched to step scanning: with a step size of 0.02 ° and a counting time of 1.5 seconds. The results were quite good.

XRD analysis

Calculation results of residual austenite:


XRD analysis

It is possible to measure phases with a content of less than 1% using the D/max 2500 diffractometer in physics. However, the scanning time should be appropriately extended, that is, a lower scanning speed should be used. Step scanning can obtain ideal results.


How to use XRD to detect substances with low content?
First, scan at a faster speed. When there are some seemingly ambiguous trace peaks in the spectrum, switch to scanning at a slower speed. According to experience, if you can see the "shadow" of a certain phase at 8 degrees per minute, there is not much improvement at a speed of 4 degrees per minute. It is necessary to switch to a speed of 1 degree/min or slower in order to have an effect. Another frequently overlooked factor is the size of the sample. Especially for bulk samples, the sample frame should be filled as much as possible to increase the irradiation volume, which is equivalent to prolonging the scanning time. Samples that can be made into powder should be made into powder as much as possible and compacted as much as possible.


SAT NANO is a best supplier of nano powder and micro powder in China, we can offer metal powder, alloy powder, oxide powder and carbide powder. We also can supply the XRD, SEM, MSDS of product that your enquiried. If you have any enquiry, please feel free to contact us at admin@satnano.com

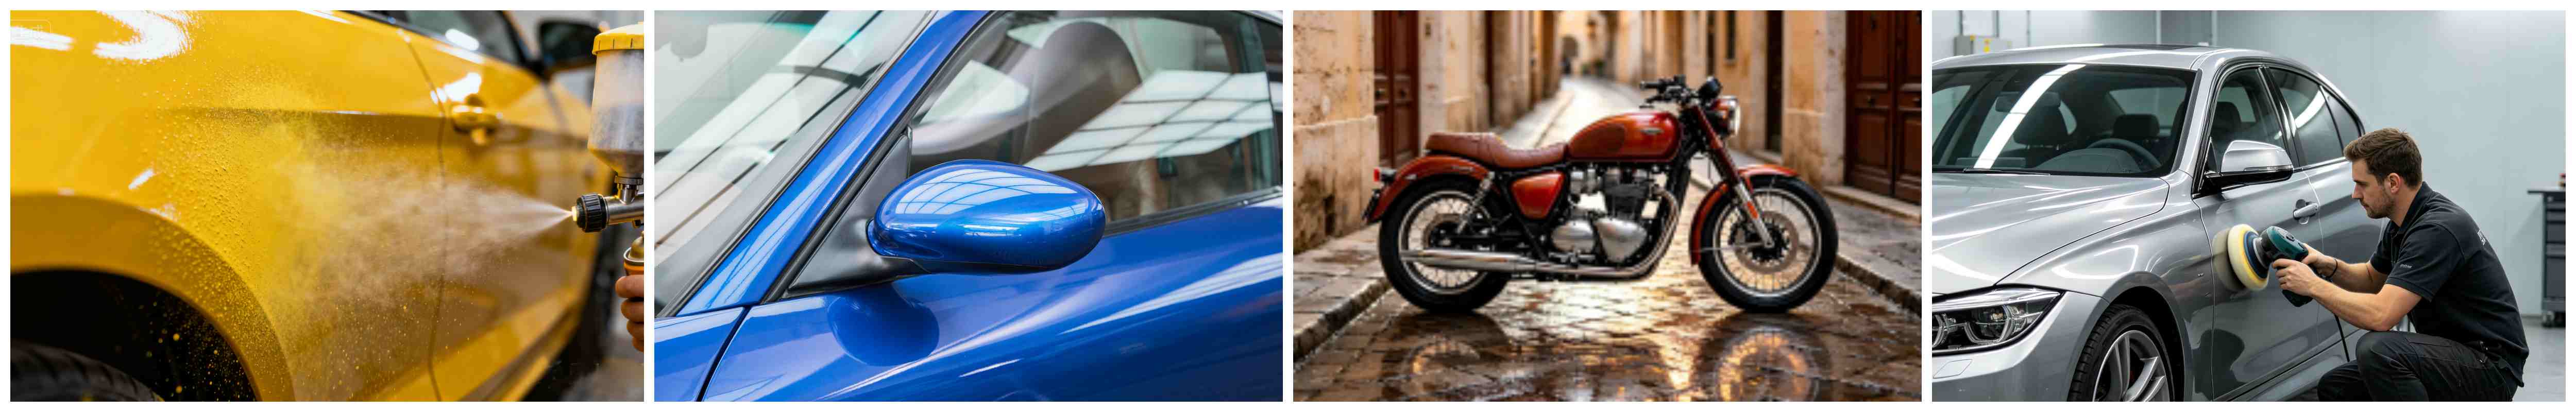
In the automotive coatings industry, every link—from the mirror-like gloss of a new car on the production line, to the fast turnaround of repair paints, and the precise delivery of personalized colors—places stringent demands on additive performance. As a high-performance synthetic aldehyde resin, Kabasph® Aldehyde Resin SH-98S, with its high gloss, high hardness, and excellent yellowing resistance, is delivering a solution that combines performance and cost-effectiveness across four core application scenarios in automotive coatings.

Aldehyde Resin A81

Key Technical Specifications and Positioning

Kabasph® Aldehyde Resin SH-98S is a white to light yellow transparent solid granular resin with the following key technical specifications:

Parameter

Typical Value

Test Method

Softening Point

90–105°C

ISO 4625-1:2004

Gardner Color (50% solution)

< 1

ISO 4630-1:2004

Acid Value

≤ 3 mgKOH/g

ISO 2114:2004

Hydroxyl Value

50–80 mgKOH/g

DIN 53240-2:1998

Density

1.10 ± 0.05 g/cm³

ISO 1183-1:2004(E)B


Notably, Kabasph® Aldehyde Resin SH-98S maintains consistency with BASF's Laropal® A 81 in most specifications while offering a broader hydroxyl value range (50–80 vs. approximately 40), providing greater formulation flexibility. In universal colorant applications, material costs can be reduced by over 30% compared to similar imported products—a significant advantage for paint manufacturers pursuing cost-effectiveness.


Scenario 1: Automotive OEM Coatings – The Hardness and Weathering Cornerstone in Baking Systems

OEM coatings represent the most important protective layer in a vehicle's lifecycle, enduring high-temperature baking on the production line and long-term exposure to UV radiation and climatic erosion. Kabasph® Aldehyde Resin SH-98S contributes to OEM coatings in three core aspects:

Hardness and Scratch Resistance: Participates in the baking crosslinking network to enhance film surface hardness, effectively reducing scratch defects during assembly line handling.

Gloss Enhancement: Its high refractive index imparts a deep mirror-like effect to the paint surface, meeting OEMs' stringent appearance standards for new vehicles.

Weathering Improvement: Excellent light and thermal stability significantly retard UV-induced yellowing and chalking, ensuring long-lasting color durability even after years of outdoor exposure.

For OEM formulators, SH-98S offers stable performance gains within the recommended addition range without requiring major alterations to existing processes.


Scenario 2: Automotive Refinish Paints – A Fast-Drying Solution for Time-Sensitive Quality Repair

Recommended Addition Level: 2%–6%

Refinish paints directly face the pressing reality of "time is money" in repair workshops. SH-98S precisely addresses three major pain points in this scenario:

Reduced Drying Time: Accelerates solvent release and physical drying, particularly effective in low-temperature or high-humidity spot repairs, helping shops improve turnaround efficiency.

Gloss and Hardness Matching: Ensures good visual and physical integration between the repaired area and the original OEM paint in terms of gloss and hardness, avoiding a "patched" appearance.

Weathering Consistency: Since repair areas often have uneven film thickness and can become weak points for aging, the Aldehyde Resin SH-98S's weathering contribution effectively narrows the lifespan gap between the repaired zone and the surrounding paint.

The product is applicable in various refinish systems including nitrocellulose, polyurethane, and amino baking enamels. Its broad compatibility allows performance upgrades without significant reformulation efforts.


Scenario 3: Motorcycle / Bicycle Paints – High Fullness Requirements for Small Surfaces

Recommended Addition Level: 2%–6%

Although motorcycles and bicycles have smaller coated areas than automobiles, users are equally sensitive to color vibrancy, film fullness, and outdoor weathering performance. Our Aldehyde Resin SH-98S plays a direct role here:

Enhanced Fullness: Improves film leveling, giving curved components like frames and fuel tanks a rich, rounded visual effect that significantly elevates product grade.

Weathering Assurance: As two-wheelers are often parked outdoors, SH-98S effectively inhibits chalking and gloss loss, maintaining color freshness over years of use.


Scenario 4: Universal Colorants (Grinding Resins) – A Cost-Reducing, Efficiency-Boosting Dispersion Engine

Recommended Addition Level (liquid formulation): 30%–60%

This is arguably SH-98S's most transformative application. As a grinding resin, it delivers a dual breakthrough:

Dispersion Efficiency and Storage Stability: With excellent pigment wetting properties and low solution viscosity, SH-98S effectively reduces milling time, prevents pigment flocculation and re-agglomeration, and ensures consistent color strength and viscosity even after long-term storage.

Significant Cost Reduction: While delivering performance comparable to imported alternatives, material costs can be lowered by over 30%—a tangible margin improvement for colorant producers.

A81 for automotive paint and OEM paint


Conclusion: Performance and Economic Value Across the Entire Value Chain

From OEM coatings on new car production lines, to fast-drying refinish paints at repair terminals, to the delicate finishes on two-wheelers, and even the upfront preparation of colorants—Kabasph® Aldehyde Resin SH-98S provides differentiated solutions for the entire automotive coatings value chain from a single core chemistry platform. Its technical equivalence to Laropal® A 81, combined with significant cost advantages, makes it an ideal choice for automotive coating manufacturers pursuing both quality excellence and cost optimization.

In automotive coating systems, a high-performance film must do more than just look stunning—it must also withstand the harshest environmental challenges, resist chemical attack, ensure flawless application, and deliver uncompromising durability over the long haul. As automotive finishing technologies advance—particularly in premium refinish, interior trim, plastic components, and high-end topcoats—CAB (Cellulose Acetate Butyrate) has earned its place as a value-driving functional resin that formulators increasingly rely on.


What does CAB resin do in automotive paint? CAB functions as a versatile performance enhancer—fine-tuning leveling, boosting gloss, accelerating drying, preventing sagging, and unlocking superior pigment dispersion. The result? Coatings that not only look exceptional but also perform reliably, coat after coat.

 Cellulose acetate butyrate factory Supplier

Selecting the right CAB grade for your automotive application, however, is anything but one-size-fits-all. It demands a deep understanding of your specific end-use requirements and formulation dynamics—and that's where informed expertise makes all the difference.


The first step in CAB selection isn't poring over technical data sheets—it's pinpointing the pain points in your formulation. In automotive coatings, CAB delivers core value across several key dimensions:


Ⅰ. What's your formulation's biggest headache—and can CAB cure it?

Fast drying: CAB significantly shortens the tack-free time of coating films. Data shows that incorporating CAB into acrylic polyol clearcoats can reduce dust-free drying time by approximately 25%. This is especially critical in refinish applications—where body shops lack the high-temperature baking ovens used in OEM lines—because faster drying directly translates to higher throughput and quicker job turnaround.


Metallic pigment orientation: CAB promotes the parallel alignment of aluminum flakes and pearlescent pigments within the film, enhancing the flop effect (color travel) and giving metallic finishes a richer, more premium visual appearance.


Resist lifting: In basecoat systems, CAB acts as a barrier against solvent penetration from the overlying clearcoat, preventing the base layer from being "lifted" or swollen—a common cause of mottled or uneven color appearance.


Improved leveling and defect reduction: Functioning as a leveling aid, CAB minimizes surface imperfections such as cratering and orange peel, while boosting distinctness of image (DOI) for a mirror-like finish.


Weather resistance and anti-yellowing: CAB is inherently UV-stable, ensuring that clearcoats remain water-white and color-true over time—a non-negotiable requirement for automotive exterior finishes.


Ⅱ. How to know the key parameters of CAB?


The CAB grade designation—such as CAB-381-0.5—is itself the very first piece of information you need for selection, as it reveals the resin's three core parameters:

1. Butyryl Content – Dictates hardness and compatibility

A higher butyryl content (e.g., the 551 series) delivers greater flexibility and broader compatibility with most coating resins, making it an ideal partner in versatile formulations. A lower butyryl content (e.g., the 171 series), on the other hand, yields higher film hardness and enhanced chemical resistance—perfect for applications where durability takes priority.


2. Hydroxyl Content – Determines reactivity

High-hydroxyl grades can crosslink with curing agents to form a denser, more robust polymer network, offering superior film integrity. Low-hydroxyl grades remain more stable and are better suited for non-crosslinking systems, where simplicity and consistency are key.


3. Viscosity – Impacts application solids and leveling

Low-viscosity grades (e.g., CAB-551-0.01) enable high-solids, low-VOC formulations without compromising flow, supporting modern environmental compliance. High-viscosity grades (e.g., CAB-381-20) provide superior rheological control and sag resistance, ensuring consistent film build even on vertical surfaces.


Ⅲ. Which CAB grade is right for your automotive application? One table tells it all.

The table below outlines the most commonly used grades and their selection criteria for typical automotive coating scenarios:


Application Scenario

Recommended Grade

Key Advantages & Critical Data

Typical Use

Primer / Metallic Paint

CAB-381-0.5

Versatile First Choice. Butyryl content 38%, balanced viscosity, offering good hardness, compatibility, and pigment orientation.

Improves parallel alignment of aluminum and pearlescent pigments, enhancing metallic effect and flop index.

CAB-321-0.1

Specialized for Re-solvent Resistance. Butyryl content 32.5%, low molecular weight, excellent re-solvent resistance.

Protects the basecoat layer from solvent penetration by the clearcoat, preventing color mottling.

CAB-381-2

Higher Hardness Control. Higher viscosity, provides superior film hardness and pigment orientation control.

Used in basecoats or intermediate coats requiring higher hardness.

Refinish / General Modification

CAB-551-0.01

Ultra-Low Viscosity Leveling Agent. Lowest Tg, excellent compatibility.

Significantly improves leveling, reduces cratering, and shortens tack-free time. Often used as a modifying additive.

CAB-551-0.2

High-Compatibility Modifier. High butyryl content (~52%), good flexibility.

Used in high-solids or UV-curable systems to improve flexibility and leveling.

High-Durability Topcoat/Clearcoat

CAB-553-0.4

High-Hydroxyl Crosslinkable Type. Alcohol-soluble, high hydroxyl content for crosslinking reactions.

Provides high crosslink density, significantly enhancing chemical resistance and weatherability.

Rheology Control / Sag Prevention

CAB-381-20

High-Viscosity Rheology Modifier. High viscosity, primarily used as a rheological control agent.

Adjusts paint viscosity to prevent sagging during vertical or thick-film application, improving workability.

Automotive Plastic Component Coatings

CAB-531-1

High Flexibility. High butyryl content (~50%), adapts to plastic deformation without excessive plasticizers.

Used for coatings on bumpers, interior parts, and other plastic substrates, providing good flexibility and adhesion.


Ⅳ. Critical Practical Formulation Tips


  • Blending is Standard Practice
    In actual formulations, to simultaneously meet leveling, sag control, and hardness requirements, grades with different viscosities are often blended. For example, use CAB-381-0.5 for primary performance, with a small addition of CAB-381-20 to adjust viscosity and prevent sagging.


  • Solvent Selection and Dissolution Safety

CAB is generally readily soluble in esters (e.g., butyl acetate) and ketones. To avoid precipitation, it is recommended to first dissolve the CAB thoroughly in strong solvents before adding hydrocarbon diluents. A classic dissolution formula is: 50% Butyl Acetate / 35% Xylene / 15% Isobutanol.


  • Moisture Prevention is Crucial
    CAB powder is hygroscopic. For moisture-sensitive polyurethane systems, dry the CAB or azeotropically dehydrate it with solvents before use to prevent bubbling in the film.
Cellulose acetate butyrate for Automotive paints and coatings

Summary

The core logic for selecting CAB is: Identify your formulation's primary objective (metallic orientation, fast drying, re-solvent resistance, or rheology control?), then understand the three key parameters of the grade (butyryl content, hydroxyl content, viscosity), and finally make the choice based on your specific application scenario. There is no "universal grade," but by following this systematic comparison and utilizing blending techniques, you can develop automotive coating solutions with excellent performance and processability. Welcome to contact us for CAB grade selection recommendations and testing methods.


-
PA6-LGF30 Automotive Fan Shrouds | Long Glass Fiber Reinforced PA6 for Engine Cooling Systems

PA6-LGF30 Automotive Fan Shrouds for Lightweight & High-Performance Cooling Systems

Long glass fiber reinforced PA6 engineered for strength, durability, and efficient automotive cooling applications.

1. Why Automotive Fan Shrouds Matter

The fan shroud is an essential component of an automotive engine cooling system. It directs airflow through the radiator, improving cooling efficiency while protecting the cooling fan from external damage.

As modern vehicles become lighter and more energy-efficient, manufacturers are replacing traditional materials with high-performance engineering plastics capable of delivering superior mechanical performance without increasing weight.

2. Why Choose PA6-LGF30?

2.1 Long Glass Fiber Reinforcement

PA6-LGF30 combines Polyamide 6 with 30% long glass fibers, creating a reinforced internal structure that provides significantly higher stiffness and impact resistance compared with conventional short glass fiber reinforced materials.

2.2 Performance Advantages

  • Excellent stiffness and structural strength
  • Outstanding impact resistance
  • High heat resistance for engine compartment environments
  • Superior dimensional stability
  • Reduced vibration and noise
  • Excellent fatigue resistance during long-term service
  • Supports automotive lightweighting initiatives

3. Engineering Challenges of Fan Shrouds

3.1 High Temperature Environment

Fan shrouds are continuously exposed to elevated temperatures generated by the engine and radiator. Materials must maintain stiffness and dimensional accuracy even after long-term thermal exposure.

3.2 Dynamic Mechanical Loads

Vehicle vibration, road impact, and continuous airflow generate repeated mechanical loading. PA6-LGF30 provides excellent fatigue performance, ensuring reliable long-term operation.

3.3 Dimensional Precision

Maintaining the correct clearance between the fan blades and shroud is critical for cooling efficiency and noise reduction. Long glass fiber reinforcement minimizes warpage and improves dimensional stability.

4. Why Long Glass Fiber Performs Better

Unlike conventional short glass fiber reinforced plastics, long glass fibers form a continuous reinforcing network inside the polymer matrix. This allows stress to be distributed more evenly throughout the component, improving impact strength, fatigue life, and overall structural integrity.

Compared with Short Glass Fiber Materials:
  • Higher impact strength
  • Improved creep resistance
  • Better fatigue durability
  • Lower warpage
  • Greater design freedom for complex injection molded parts

5. Typical Applications

  • Automotive radiator fan shrouds
  • Electric cooling fan housings
  • HVAC air guide components
  • Engine compartment structural parts
  • Electric vehicle cooling system components

6. About Xiamen LFT Composite Plastics

6.1 Long Fiber Composite Material Manufacturer

Xiamen LFT Composite Plastics Co., Ltd. specializes in manufacturing long glass fiber reinforced thermoplastic materials, including PP, PA6, PA66, TPU, PPS, PPA, and long carbon fiber reinforced composite materials for demanding engineering applications.

6.2 Industries We Serve

Our materials are widely used in automotive, new energy vehicles, power tools, industrial equipment, consumer electronics, and structural engineering applications requiring lightweight design and exceptional mechanical performance.

7. Why Choose Our PA6-LGF30?

  • Over 20 years of long fiber composite manufacturing experience
  • Consistent fiber length for superior mechanical performance
  • Customized formulations available
  • Global technical support
  • Ideal for automotive lightweight solutions

8. Contact Us

Looking for high-performance PA6-LGF30 materials for automotive applications?

Contact us for technical datasheets, material recommendations, sample evaluation, and engineering support.

Contact Us
-

As global temperatures continue to rise, air conditioners have become an essential part of everyday life. The recent heatwaves across Europe have triggered a surge in air conditioner demand, placing greater emphasis on product performance, durability, and quiet operation.

Behind every high-performance air conditioner lies more than an efficient compressor or an advanced control system—the choice of material plays a critical role. To meet the growing demand for lightweight, low-noise, and long-lasting HVAC systems, engineering plastics are increasingly replacing traditional metal components in fan impellers, blower housings, motor brackets, structural frames, and other key parts.
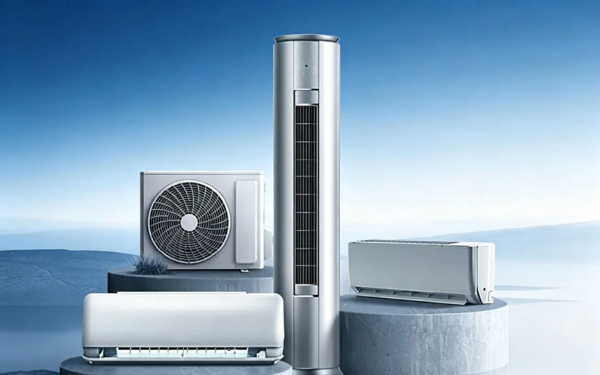
Engineering Plastics for Air Conditioners

So, which engineering plastics are most commonly used in air conditioners? What advantages does each material offer? And why are high-stiffness long glass fiber reinforced thermoplastics (LFT) becoming the preferred choice for next-generation HVAC components?

In this article, we'll explore the most widely used engineering plastics in air conditioners and explain how high-performance composite materials help reduce noise and vibration, improve structural strength, and enhance the overall efficiency and reliability of modern air conditioning systems.

Challenges in Selecting Engineering Plastics for Air Conditioners

Material selection plays a critical role in the design and performance of modern air conditioning systems. Beyond manufacturing costs, the right engineering plastic directly affects product durability, structural strength, noise levels, and long-term reliability. However, selecting the optimal material is not always straightforward. Air conditioner manufacturers typically face two major challenges:

1. Complex Material Selection

A wide range of engineering plastics—including PP, ABS, PA, PBT, PPS, and long glass fiber reinforced thermoplastics (LFT)—offer different advantages in terms of mechanical strength, heat resistance, dimensional stability, processability, and cost. Choosing the most suitable material for each component requires balancing application requirements with performance and budget. An inappropriate material choice can lead to increased noise and vibration, reduced service life, or unnecessary manufacturing costs.

2. Balancing Multiple Performance Requirements

Modern air conditioners demand materials that provide high stiffness while also delivering excellent heat resistance, flame retardancy, fatigue resistance, dimensional stability, and efficient injection molding performance. At the same time, manufacturers must achieve lightweight designs, maintain cost efficiency, and ensure high production productivity. Finding the right balance among these competing requirements remains one of the biggest challenges in HVAC material selection.
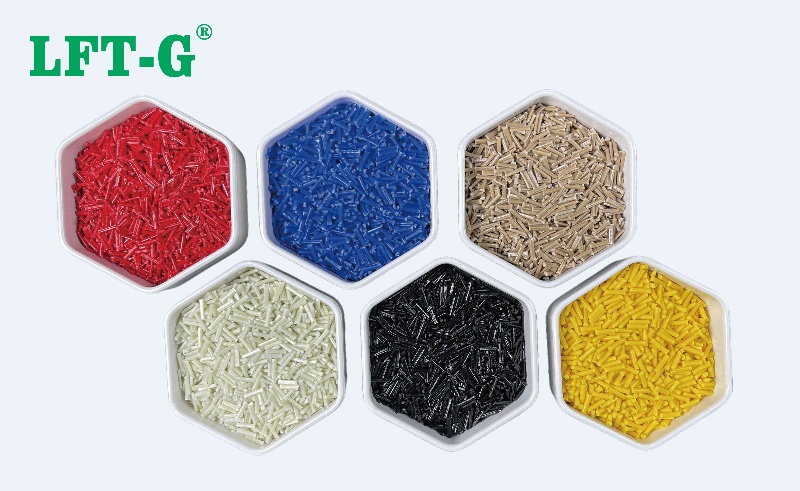
HVAC Material Selection

Engineering Plastics Used in Air Conditioners

01. ABS – The Preferred Material for Exterior Components

Typical Applications

ABS is widely used for visible exterior parts such as front panels, control panels, decorative covers, and other cosmetic components. These parts are the first elements consumers notice, making appearance, surface quality, and durability key design considerations.

Key Advantages

ABS offers an excellent surface finish with high gloss, making it ideal for premium-looking air conditioner housings. Its outstanding paintability also allows manufacturers to achieve a wide range of colors, textures, and decorative effects to meet different product designs.

In addition, ABS provides excellent impact resistance, helping exterior components withstand daily handling, accidental impacts, and long-term use while maintaining their appearance. Its good processability and cost-effectiveness have made ABS one of the most widely used engineering plastics for air conditioner exterior applications.

02. PP and Modified PP – The Cost-Effective Choice for Functional Components

Typical Applications

Polypropylene (PP) is widely used for non-load-bearing components such as air filters, drain pans, internal brackets, and various functional parts. While these components are not highly visible, they play an essential role in ensuring the reliable operation of the air conditioning system.

Key Advantages

PP offers excellent low-temperature toughness and good chemical resistance, allowing it to withstand moisture, cleaning agents, and a wide range of operating environments. Its low density, easy processability, and competitive cost make it one of the most economical engineering plastics for high-volume air conditioner production.

Why Modify PP?

Standard PP can be further enhanced with glass fiber reinforcement, flame-retardant additives, or mineral fillers to meet more demanding performance requirements. Modified PP delivers significantly higher stiffness, improved dimensional stability, enhanced heat resistance, and better flame-retardant performance while maintaining the cost advantages of conventional PP. As a result, it has become a preferred material for many structural and functional HVAC components where strength, safety, and cost efficiency must be carefully balanced.
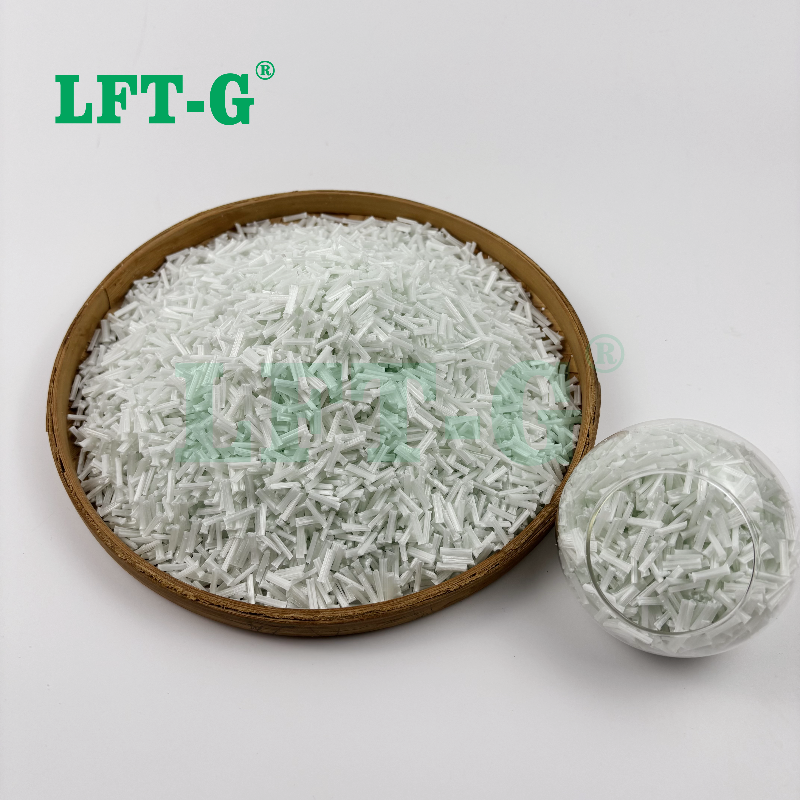
PP Long Glass Fiber Reinforced Material

PP Long Glass Fiber Reinforced Thermoplastic (LGF-PP)

03. PC/ABS Alloy – The Balanced Solution for Premium Air Conditioners

Typical Applications

PC/ABS alloy is commonly used for structural parts and exterior housings in premium air conditioners, especially for thin-wall components that require both strength and an excellent surface finish.

Key Advantages

By combining the strengths of polycarbonate (PC) and ABS, PC/ABS offers better heat resistance and impact strength than ABS while providing easier processing and lower manufacturing costs than pure PC. This balance of mechanical performance, appearance, and processability makes it an ideal material for high-end HVAC applications.

04. PA (Polyamide) – The Core Material for High-Performance Structural Components

Typical Applications

Polyamide (PA), particularly glass fiber reinforced grades such as PA6 GF30, is widely used for fan blades, motor brackets, bearing supports, and other structural components exposed to continuous vibration, mechanical loads, and elevated temperatures.

Key Advantages

PA provides outstanding mechanical strength, wear resistance, and creep resistance, ensuring long-term structural stability under demanding operating conditions. It also maintains excellent performance across a wide temperature range, typically from -30°C to 120°C, making it well suited for air conditioner components that require long service life and reliable operation.

05. PBT and PET – Reliable Materials for Electrical and High-Temperature Applications

PBT: Ideal for Electrical Components

PBT is widely used in electrical control boxes, connectors, terminal blocks, and other components requiring excellent electrical insulation. It also offers fast injection molding cycles, good dimensional stability, and reliable performance under continuous thermal exposure, making it a preferred material for electrical applications in HVAC systems.

Reinforced PET: Built for High-Temperature Environments

Glass fiber reinforced PET is commonly used in air outlets, coil supports, and other components exposed to elevated temperatures. With excellent heat resistance—typically exceeding 200°C for reinforced grades—along with high stiffness and dimensional stability, reinforced PET ensures reliable performance in demanding thermal environments.

06. PU (Polyurethane) – The Key to High-Efficiency Thermal Insulation

Typical Applications

Polyurethane (PU) foam is widely used as the thermal insulation material between the inner and outer shells of air conditioners, filling cavities to improve thermal efficiency while also providing structural support.

Key Advantages

PU features an extremely low thermal conductivity, effectively minimizing heat transfer and reducing cooling energy loss. Its excellent insulation performance helps improve the overall energy efficiency of air conditioning systems while contributing to quieter operation and enhanced long-term durability.
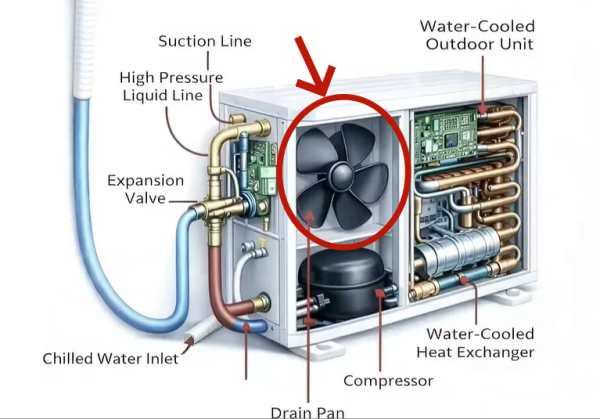
Engineering Plastics Used in Air Conditioners

Advantages of Engineering Plastics for Air Conditioner Applications

Compared with general-purpose plastics, engineering plastics offer superior mechanical strength, heat resistance, flame retardancy, dimensional stability, and long-term reliability. These properties enable manufacturers to produce air conditioners that are lighter, quieter, more durable, and more energy efficient.

Each material offers unique advantages for different applications. ABS is ideal for exterior components, PA excels in high-load structural parts, while modified PP, PBT, PET, and PC/ABS are widely used in electrical and functional components. Selecting the right material for each application is essential to achieving the best balance between performance, manufacturability, and cost.

Why Choose Long Glass Fiber Reinforced Thermoplastics (LFT)?

As air conditioners continue to evolve toward lightweight, low-noise, and high-performance designs, Long Glass Fiber Reinforced Thermoplastics (LFT) have become an ideal material for structural HVAC components. Compared with conventional reinforced plastics, LFT offers higher stiffness, better impact resistance, improved vibration damping, and superior dimensional stability.

At Xiamen LFT Composite Plastics Co., Ltd., we provide high-performance PP-LGF, PA6-LGF, PA66-LGF, PPA-LGF, PPS-LGF, and customized LFT solutions to help HVAC manufacturers improve product performance, reduce noise and vibration, and achieve lightweight designs.
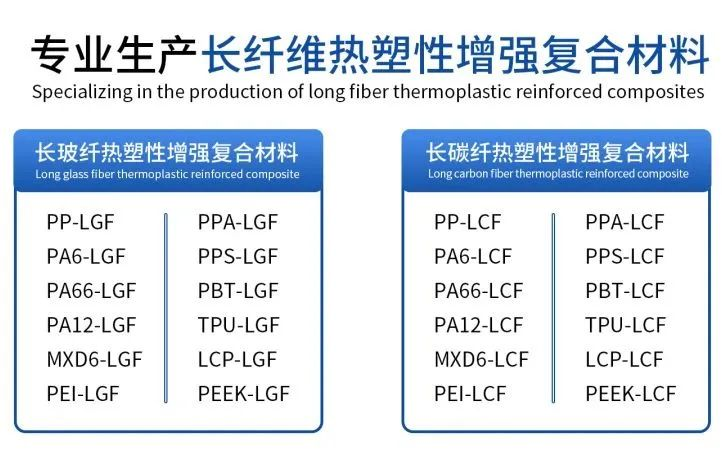
Long Glass Fiber Reinforced Thermoplastics for Air Conditioners
-
-

How to Choose the Right Glass Fiber Content for PA66

A Practical Guide to Balancing Mechanical Performance, Heat Resistance, Processability and Cost

Introduction

Glass fiber reinforced PA66 (GF PA66) is one of the most widely used engineering plastics in automotive, electrical, industrial machinery and structural applications. By incorporating glass fibers into Nylon 66, manufacturers can significantly improve strength, stiffness, dimensional stability and heat resistance.

However, one question frequently arises during material selection:

Should you choose 20%, 30%, 40%, 50% or even 60% glass fiber reinforced PA66?

Many engineers assume that higher glass fiber content always means better performance. In reality, increasing glass fiber improves certain properties while reducing others, such as impact resistance and flowability.

Selecting the proper glass fiber percentage requires balancing mechanical performance, molding process, product design and overall manufacturing cost.


How Glass Fiber Content Influences PA66 Performance

Glass fibers function as reinforcement within the PA66 matrix. As fiber loading increases, the reinforcing network becomes stronger, enabling the composite to withstand higher mechanical loads and elevated temperatures.

At the same time, excessive glass fiber loading may introduce processing challenges and reduce toughness.

1. Mechanical Strength and Stiffness Increase

The most obvious benefit of adding glass fiber is the improvement of mechanical properties.

  • Higher tensile strength
  • Higher flexural strength
  • Higher modulus
  • Improved rigidity
  • Better dimensional stability

For structural components subjected to continuous loads, increasing glass fiber content often provides significant performance advantages.

2. Heat Resistance Improves

Glass fibers restrict polymer chain movement, resulting in improved heat deflection temperature (HDT) and long-term thermal stability.

This makes high glass fiber PA66 ideal for automotive engine compartments, electrical components and industrial equipment operating at elevated temperatures.

3. Flowability Decreases

As glass fiber loading increases, melt viscosity rises during injection molding.

Consequently:

  • Injection pressure increases
  • Thin-wall filling becomes more difficult
  • Surface fiber exposure becomes more noticeable
  • Complex mold designs require careful optimization

4. Impact Toughness Gradually Decreases

Higher rigidity generally comes at the expense of toughness.

Compared with lower glass fiber grades, high glass fiber PA66 exhibits reduced elongation and lower impact resistance, making it less suitable for components exposed to repeated impacts.

5. Processing Difficulty and Cost Increase

Higher glass fiber content usually means:

  • Greater mold wear
  • Higher machine requirements
  • More difficult processing window
  • Higher raw material cost

Therefore, the highest glass fiber percentage is not always the most economical solution.


Typical Glass Fiber Content Ranges

Glass Fiber Content Characteristics Typical Applications
10–20% Balanced mechanical properties, good flowability, easy processing, economical. Consumer products, electrical housings, light-duty structural components.
25–30% Excellent balance between strength, stiffness and processability. Automotive components, power tools, appliance structures.
30–40% High rigidity, excellent heat resistance and dimensional stability. Cooling fans, industrial machinery, motor housings.
40–50% Ultra-high stiffness with excellent structural performance. Heavy-duty structural components and precision industrial parts.
Above 50% Special engineering applications requiring maximum rigidity and wear resistance. Customized engineering solutions.

How to Select the Right Glass Fiber Content

Choosing the appropriate glass fiber content is not simply about selecting the highest strength material. Engineers should evaluate the entire product lifecycle, including mechanical requirements, molding capability, service environment and production cost.

Step 1

Define Performance Requirements

Determine the required mechanical strength, stiffness, impact resistance, heat resistance and dimensional stability before selecting a material grade.

Step 2

Balance Cost and Processability

Higher glass fiber content improves performance but also increases molding difficulty, tooling wear and material cost.

Step 3

Use Industry Experience

Reference proven material selections used in automotive, electrical and industrial applications to shorten development time.

Step 4

Prototype and Validate

Always verify mechanical properties, thermal performance and molding behavior through prototype testing before mass production.


Recommended Glass Fiber Content by Industry

Industry Typical Components Recommended GF Content
Automotive Engine covers, brackets, housings, cooling system components 20–30%
Industrial Machinery Structural parts, gears, support frames 25–40%
Electrical & Electronics Connectors, switches, electrical housings 15–25%
Cooling Fans Fan blades, motor housings 30–50%
Precision Engineering High-load structural components 30–60%

Why Long Glass Fiber Reinforced PA66 Performs Better

Although conventional short glass fiber reinforced PA66 is widely used, many demanding engineering applications are now transitioning to Long Glass Fiber Reinforced PA66 (LGF PA66).

Compared with short glass fiber materials, long glass fiber composites retain significantly longer fiber lengths after injection molding, creating a stronger reinforcing network inside the polymer matrix.

Property Short Glass Fiber PA66 Long Glass Fiber PA66
Impact Strength Good Excellent
Fatigue Resistance Moderate Outstanding
Dimensional Stability Good Excellent
Long-term Mechanical Performance Good Superior
Lightweight Replacement of Metal Limited Highly Suitable

LFT-G® Long Glass Fiber PA66 Solutions

LFT-G specializes in long fiber reinforced thermoplastic composites for demanding engineering applications.


Frequently Asked Questions

Is higher glass fiber content always better?

No. While higher glass fiber content improves stiffness and heat resistance, it also reduces flowability and impact toughness while increasing manufacturing cost.

What is the most commonly used glass fiber percentage?

Glass fiber contents between 30% and 40% offer an excellent balance between strength, processing performance and cost, making them the most widely used grades.

When should I choose 40% or higher glass fiber reinforced PA66?

High glass fiber grades are recommended for structural components requiring maximum stiffness, high temperature resistance and long-term dimensional stability.

Why choose long glass fiber reinforced PA66?

Long glass fiber reinforced PA66 provides superior impact strength, fatigue resistance and structural performance compared with conventional short glass fiber materials, making it ideal for lightweight metal replacement applications.

Contact our engineering team today to receive technical data sheets, application recommendations and customized material solutions.

Request a Free Consultation
keyboard_arrow_up